

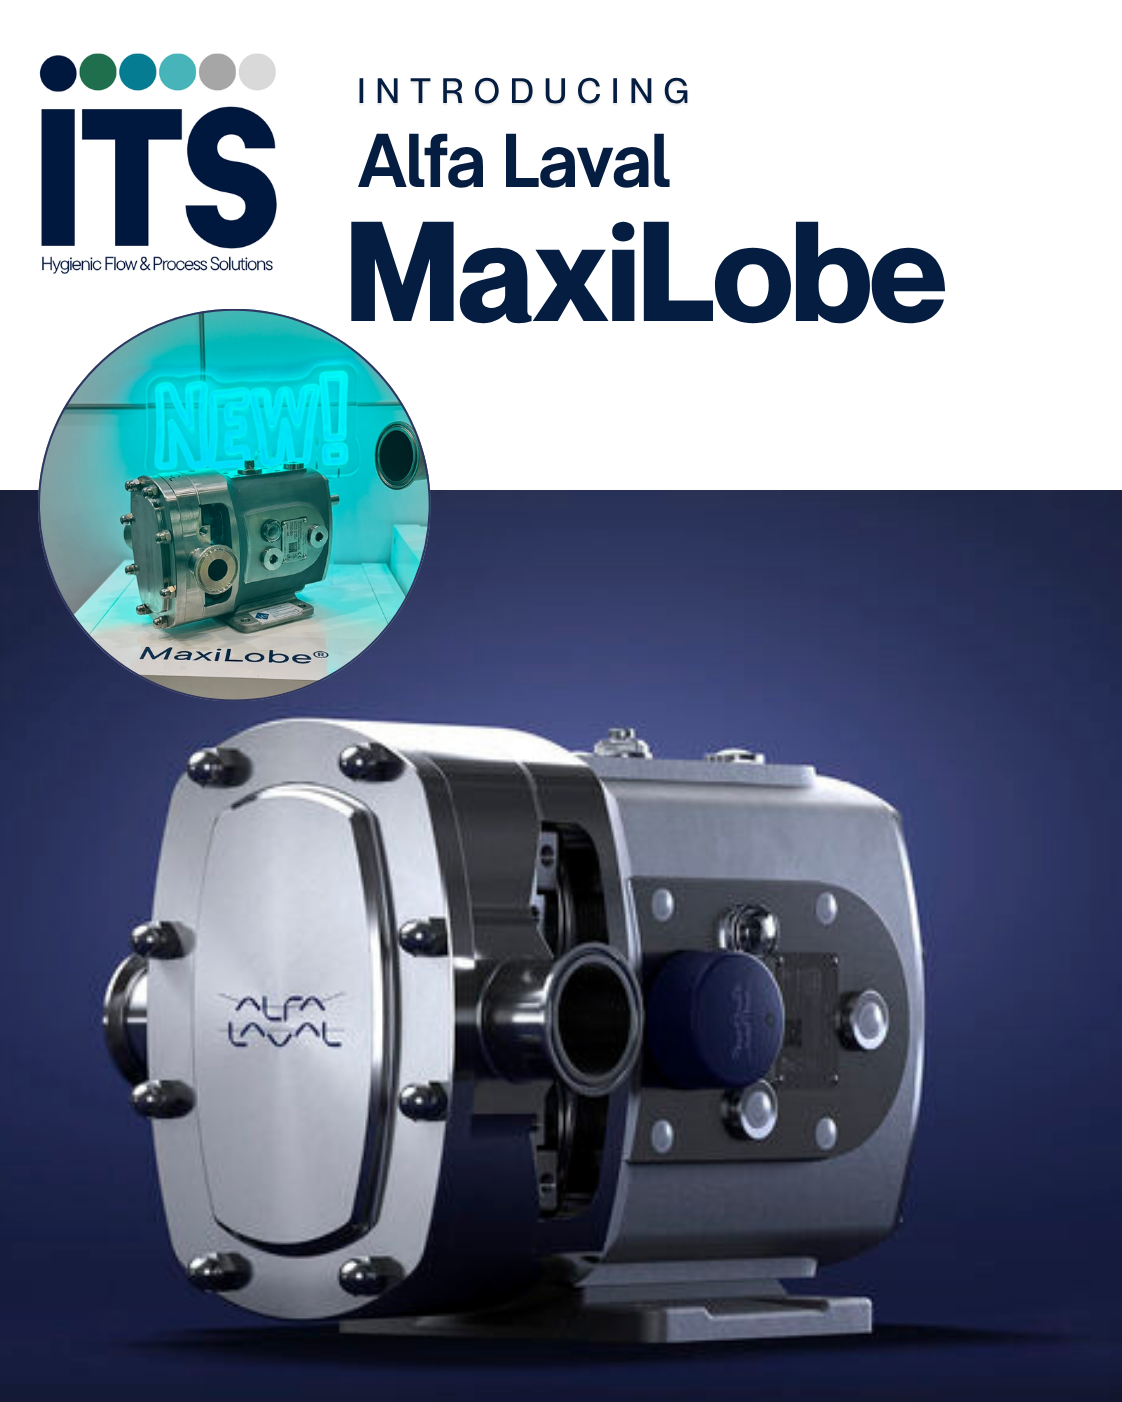
There’s exciting news from Alfa Laval! The new MaxiLobe® rotary lobe pump range has officially launched, delivering significant improvements in efficiency, uptime, product protection, and total cost of ownership for hygienic processing applications.
Designed for the dairy, food, beverage, pharmaceutical, and personal care industries, MaxiLobe builds on Alfa Laval’s proven rotary lobe pump technology with a number of key enhancements:
✅ Higher volumetric efficiency for improved performance and yield
✅ Wider operating range with flow rates up to 350 m³/hr and pressures up to 16 bar
✅ Lower operating speeds to reduce product shear and protect sensitive products
✅ Simplified maintenance with front-loading seals and easy-to-set clearances
✅ Reduced energy consumption, with some applications achieving energy savings of more than 25%
✅ Increased uptime and lower total cost of ownership
✅ Easy upgrade path from existing Alfa Laval SRU and many SX pump installations without major pipework modifications
For manufacturers looking to improve process efficiency while maintaining product quality, MaxiLobe offers the opportunity to achieve the same duty with a smaller, more efficient pump, reducing both capital and operating costs.
At ITS, you can purchase the new Alfa Laval MaxiLobe range with full technical support from our experienced team. From pump selection and sizing through to application advice and ongoing servicing support, we’re here to help ensure you get the right solution for your process.
📞 01675 465191
📧 sales@industrialtradingsolutions.com
Looking to upgrade an existing rotary lobe pump or specify a new hygienic pumping solution? Get in touch with the ITS team today.
#AlfaLaval #MaxiLobe #RotaryLobePump #PumpTechnology #FoodManufacturing #DairyProcessing #PharmaceuticalManufacturing #ProcessEngineering #FluidHandling #HygienicProcessing #ITS #DistributingSolutions #ProductLaunch
